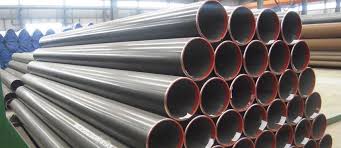
Large-diameter straight seam steel pipe manufacturers With the development of China’s national economy, large-diameter straight seam steel pipes are increasingly affected by oil and gas, slurry transportation and steel due to their high pressure bearing capacity, low resistance, low temperature resistance, corrosion resistance, and convenient installation and maintenance. Structure engineering and other industries are welcome.
The main production process description of large diameter straight seam welded pipe:
1. Stencil: After the steel plate used to manufacture the large-diameter submerged arc welded straight seam steel pipe enters the production line, the whole board ultrasonic inspection is first carried out;
2. Milling edge: double-sided milling the two edges of the steel plate by the edge milling machine to achieve the required plate width, parallelism of the edge of the plate and the shape of the groove;
3. Pre-bending: pre-bending the edge of the board with a pre-bending machine to make the edge of the board have the required curvature;
4. Molding: First, half of the pre-bent steel plate is stepped and stamped on the JCO molding machine. The large-diameter straight seam steel pipe manufacturer is pressed into a “J” shape, and the other half of the steel plate is also bent and pressed into “C”. Shape, and finally form an “O” shape of the opening
5. Pre-welding: the straight seam welded steel pipe after forming is welded and continuously welded by gas shielded welding (MAG);
6. Internal welding: welding by longitudinal multi-wire submerged arc welding (up to four wires) on the inside of a straight seam steel pipe;
7. External welding: welding by longitudinal multi-wire submerged arc welding on the outside of straight seam submerged arc welded steel pipe;
8. Ultrasonic inspection I: 100% inspection of the inner and outer welds of straight seam welded steel pipes and the base metal on both sides of the weld;
9. X-ray inspection I: 100% X-ray industrial TV inspection of internal and external welds, using image processing system to ensure the sensitivity of flaw detection;
10. Expanding diameter: Expanding the full length of the submerged arc welded straight seam steel pipe to improve the dimensional accuracy of the steel pipe and improve the distribution of stress in the steel pipe;
11. Hydraulic test: On the hydraulic test machine, the steel pipe after the diameter expansion is tested one by one to ensure that the steel pipe meets the test pressure required by the standard. The machine has automatic recording and storage functions;
12. Chamfering: the steel pipe after the inspection is qualified for pipe end processing, and the large-diameter straight seam steel pipe manufacturer meets the required pipe end groove size;
13. Ultrasonic inspection II: Ultrasonic inspection is carried out again and again to check for defects that may occur after straightening and water pressure of straight seam welded steel pipes;
14. X-ray inspection II: X-ray industrial TV inspection and tube end weld filming of the steel pipe after the expansion and hydrostatic test;
15. Tube end magnetic particle inspection: carry out this inspection to find the tube end defect;
16. Anti-corrosion and coating: The qualified steel pipe is anti-corrosion and coating according to user requirements.